
ISO 4954:2018 Annex A reference scope
Annex A covers steels not intended for heat treatment after cold working. This page reproduces the reviewed 2018 edition’s delivery-condition, cast-analysis and mechanical-property tables. The edition and requirements agreed in the order govern acceptance; these reference excerpts are not a batch certificate or a declaration that every illustrated product complies with this standard.
Creation Group provides cold-heading wire and shaped-wire material processing, testing and technical services through its Shanghai operating team and Wuhu manufacturing base. Confirm grade, product form, delivery condition and application requirements through technical review.
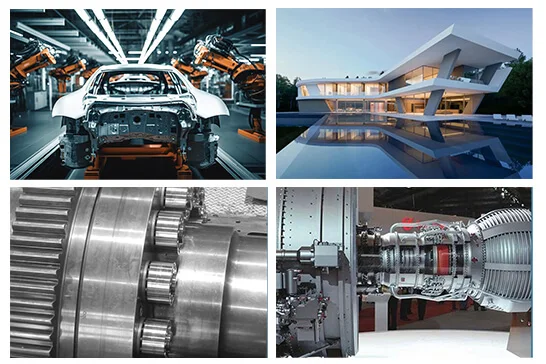
Related catalogue references
The following original catalogue illustrations and linked pages are related references; they do not establish grade equivalence or suitability for a particular component.
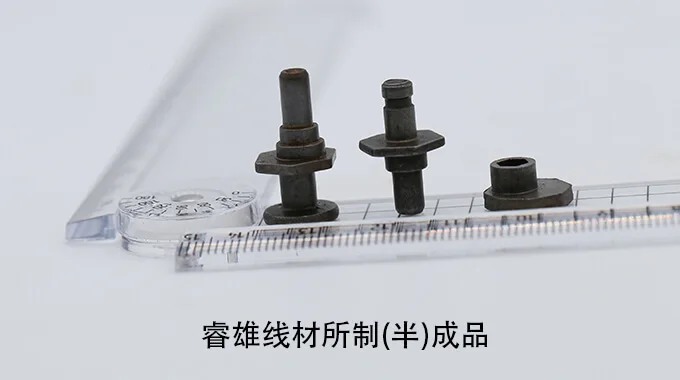
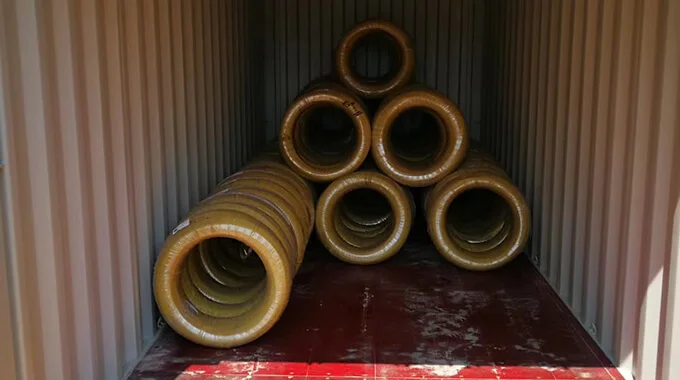
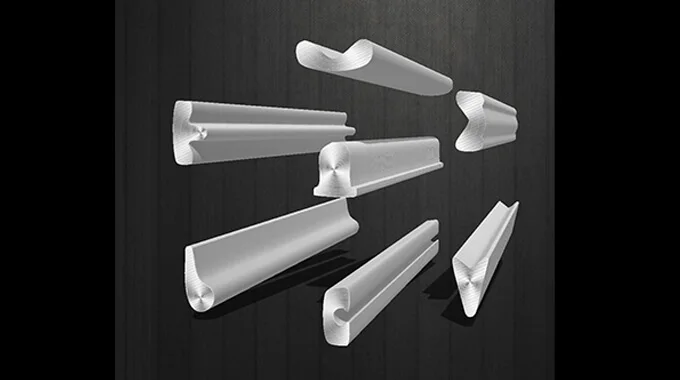
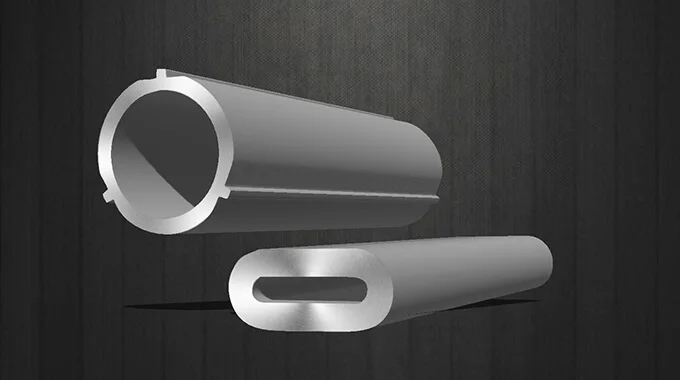
Processing illustrations
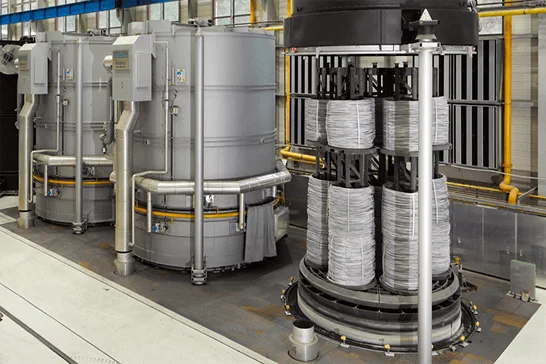
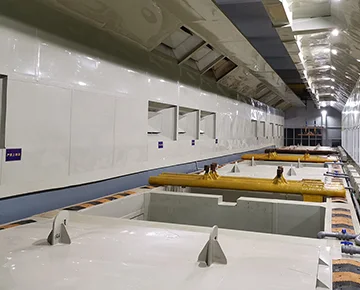
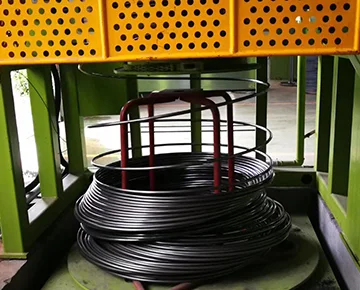
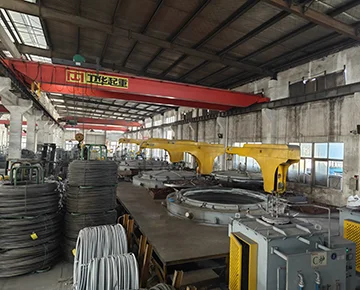
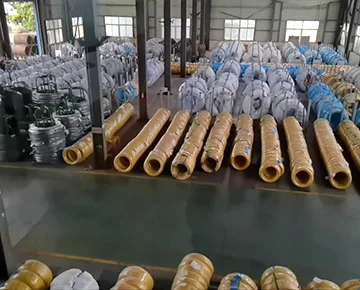
The original catalogue illustrates wire rod, surface preparation, drawing, annealing, inspection and finished material. Select the actual route for the ordered grade and delivery condition. These photographs do not establish a particular processing cycle, manufacturing history or batch result.
Source-bound technical tables
Use Table A.1 to identify the delivery condition and product form before applying Tables A.2 and A.3. Blank cells, dashes, limits and footnotes retain the distinctions in the reviewed source. Wide tables scroll horizontally on smaller screens.
1. Delivery conditions and applicable requirements
Table A.1 – Heat-treatment conditions, product forms and applicable requirements
| Delivery condition | Symbol | Wire rod | Bar | Wire |
|---|---|---|---|---|
| Untreated, as hot rolled | +AR | X | X | — |
| Untreated and peeled | +AR+PE | X | X | — |
| Untreated and cold drawn | +AR+C | — | X | X |
| Untreated, cold drawn and spheroidize annealed | +AR+C+AC | — | X | X |
| Untreated, cold drawn, spheroidize annealed and skin passed | +AR+C+AC+LC | — | X | X |
| Annealed to achieve spheroidal carbides, as treated or peeled | +AC or AC+PE | X | X | — |
| Annealed to achieve spheroidal carbides, then cold drawn | +AC+C | — | X | X |
X = applicable; — = not applicable. Chemical composition is specified in Table A.2 and mechanical properties in Table A.3. Supplementary or special requirements under Annex E apply if agreed at enquiry and order. Other delivery conditions may be agreed at the time of order. Source: ISO 4954:2018, Table A.1, page 17 (PDF page 23). The source notation “+AC or AC+PE” is retained as printed; confirm the exact delivery condition in the order.
2. Chemical composition
Table A.2 – Chemical composition by cast analysis of steels not intended for heat treatment after cold working
| Steel name | Mass fraction, %a | ||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|
| C | Si | Mn | P | S | Cr | Ni | Mo | Alb | Cu | Cr + Ni + Mo | |
| C2C | 0.03 | 0.10 | 0.20 to 0.40d | 0.020 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C4C | 0.02 to 0.06 | 0.10 | 0.25 to 0.40 | 0.020 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C8C | 0.06 to 0.10 | 0.10 | 0.25 to 0.45 | 0.020 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C10C | 0.08 to 0.12 | 0.10 | 0.30 to 0.50 | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C10GC | 0.08 to 0.12 | 0.15 to 0.25c | 0.30 to 0.50 | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | —c | 0.30 | 0.50 |
| C15C | 0.13 to 0.17 | 0.10 | 0.35 to 0.60 | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C15GC | 0.13 to 0.17 | 0.15 to 0.25c | 0.35 to 0.60 | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | —c | 0.30 | 0.50 |
| C17C | 0.15 to 0.19 | 0.10 | 0.65 to 0.85 | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C17GC | 0.15 to 0.19 | 0.15 to 0.25c | 0.65 to 0.85 | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | —c | 0.30 | 0.50 |
| C20C | 0.18 to 0.22 | 0.10 | 0.70 to 0.90d | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C20GC | 0.18 to 0.22 | 0.15 to 0.25c | 0.70 to 0.90d | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | —c | 0.30 | 0.50 |
| C25C | 0.23 to 0.27 | 0.10 | 0.80 to 1.00d | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | 0.020 to 0.060 | 0.30 | 0.50 |
| C25GC | 0.23 to 0.27 | 0.15 to 0.25c | 0.80 to 1.00d | 0.025 | 0.025 | 0.30 | 0.30 | 0.10 | —c | 0.30 | 0.50 |
Elements not listed must not be intentionally added to the steel without the purchaser’s agreement, except for finishing the heat. Appropriate precautions are required to prevent additions of elements from scrap or other production materials. Residual elements may nevertheless be present if they do not impair mechanical properties or suitability.
a Values are maximum limits unless otherwise indicated.
b Aluminium may be replaced by one or more elements with a similar effect.
c C10GC, C15GC, C17GC and C20GC may be supplied in two qualities: a) with a maximum aluminium content of 0.015%, or b) without aluminium and with silicon of 0.15 to 0.25% for hot-dip galvanizing.
d For C2C, C20C, C20GC and C25C, a lower manganese content may be specified with a range of 0.20%.
Source note: The C25GC row carries footnote markers c and d in ISO 4954:2018, but C25GC is not named in the wording of these footnotes. The markers and notes are reproduced as in the source; the conditions require clarification before application to C25GC.
3. Mechanical properties
Table A.3 – Mechanical properties of wire rod, bars and wire not intended for heat treatment after cold working
| Steel name | Diameter | Delivery condition | ||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| +AR or +AR+PE | +AC or +AC+PE | +AR+C | +AR+C+AC | +AR+C+AC+LC | +AC+C | |||||||||
| over, mm | up to and including, mm | Rm max., MPa | Za min., % | Rm max., MPa | Z min., % | Rm max., MPa | Z min., % | Rm max., MPa | Z min., % | Rm max., MPa | Z min., % | Rm max., MPa | Z min., % | |
| C2C | 2 | 5 | — | — | — | — | — | — | 310 | 80 | 350 | 75 | — | — |
| 5 | 10 | 360 | 75 | — | — | 450 | 70 | 300 | 80 | 340 | 75 | — | — | |
| 10 | 40 | 360 | 75 | — | — | 440 | 70 | 300 | 80 | 340 | 75 | — | — | |
| 40 | 100 | 360 | 75 | — | — | 440 | 68 | 300 | 80 | 340 | 75 | — | — | |
| C4C | 2 | 5 | — | — | — | — | 320 | 77 | 360 | 73 | — | — | ||
| 5 | 10 | 390 | 70 | 330 | 75 | 470 | 66 | 310 | 77 | 350 | 73 | 410 | 70 | |
| 10 | 40 | 390 | 70 | 330 | 75 | 460 | 66 | 300 | 77 | 350 | 73 | 400 | 70 | |
| 40 | 100 | 390 | 70 | 330 | 75 | — | — | — | — | — | — | — | — | |
| C8C | 2 | 5 | — | — | — | — | — | — | 350 | 72 | 390 | 68 | — | — |
| 5 | 10 | 410 | 65 | 360 | 70 | 490 | 63 | 340 | 72 | 380 | 68 | 450 | 65 | |
| 10 | 40 | 410 | 65 | 360 | 70 | 480 | 63 | 340 | 72 | 380 | 68 | 440 | 65 | |
| 40 | 100 | 410 | 65 | 360 | 70 | — | — | — | — | — | — | — | — | |
| C10C / C10GC | 2 | 5 | — | — | — | — | — | — | 370 | 72 | 410 | 68 | — | — |
| 5 | 10 | 430 | 60 | 380 | 70 | 520 | 58 | 360 | 72 | 400 | 68 | 470 | 63 | |
| 10 | 40 | 430 | 60 | 380 | 70 | 510 | 58 | 360 | 72 | 400 | 68 | 460 | 63 | |
| 40 | 100 | 430 | 60 | 380 | 70 | — | — | — | — | — | — | — | — | |
| C15C / C15GC | 2 | 5 | — | — | — | — | — | — | 390 | 70 | 430 | 66 | — | — |
| 5 | 10 | 460 | 58 | 400 | 68 | 550 | 56 | 380 | 70 | 420 | 66 | 490 | 63 | |
| 10 | 40 | 460 | 58 | 400 | 68 | 540 | 56 | 380 | 70 | 420 | 66 | 480 | 63 | |
| 40 | 100 | 460 | 58 | 400 | 68 | — | — | — | — | — | — | — | — | |
| C17C / C17GC | 2 | 5 | — | — | — | — | — | — | 430 | 67 | 470 | 63 | — | — |
| 5 | 10 | 520 | 58 | 440 | 65 | 610 | 56 | 420 | 67 | 460 | 63 | 530 | 60 | |
| 10 | 40 | 520 | 58 | 440 | 65 | 600 | 56 | 420 | 67 | 460 | 63 | 520 | 60 | |
| 40 | 100 | 520 | 58 | 440 | 65 | — | — | — | — | — | — | — | — | |
| C20C / C20GC | 2 | 5 | — | — | — | — | — | — | 470 | 67 | 510 | 63 | — | — |
| 5 | 10 | 560 | 55 | 480 | 65 | 650 | 53 | 460 | 67 | 500 | 63 | 570 | 60 | |
| 10 | 40 | 560 | 55 | 480 | 65 | 640 | 53 | 460 | 67 | 500 | 63 | 560 | 60 | |
| 40 | 100 | 560 | 55 | 480 | 65 | — | — | — | — | — | — | — | — | |
| C25C | 2 | 5 | — | — | — | — | — | — | 500 | 65 | 540 | 60 | — | — |
| 5 | 10 | 590 | 50 | 510 | 60 | 680 | 50 | 490 | 65 | 530 | 60 | 600 | 55 | |
| 10 | 40 | 590 | 50 | 510 | 60 | 670 | 50 | 490 | 65 | 530 | 60 | 590 | 55 | |
| 40 | 100 | 590 | 50 | 510 | 60 | — | — | — | — | — | — | — | — | |
| C25GC | 2 | 5 | — | — | — | — | 570 | 45 | — | — | 440 | 55 | — | — |
| 5 | 10 | 590 | 50 | — | — | 470 | 45 | — | — | 440 | 55 | 440 | 55 | |
| 10 | 40 | 590 | 50 | — | — | 470 | 45 | — | — | 440 | 55 | 440 | 55 | |
| 40 | 100 | 590 | 50 | — | — | — | — | — | — | — | — | — | — | |
| a Values are given for information only. | ||||||||||||||
Reference edition: ISO 4954:2018. These excerpts do not replace the complete standard or a delivery-batch inspection certificate. Annex A supplies no hardenability table for these grades.
Inspection equipment and example images
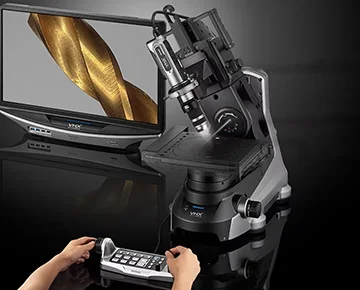
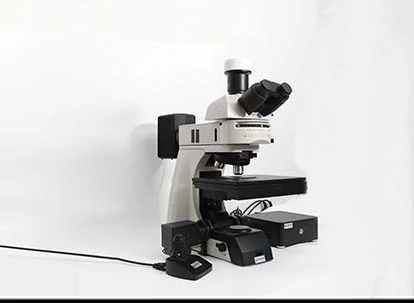
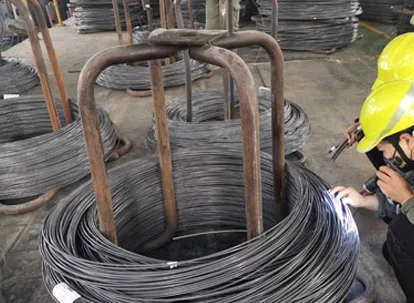
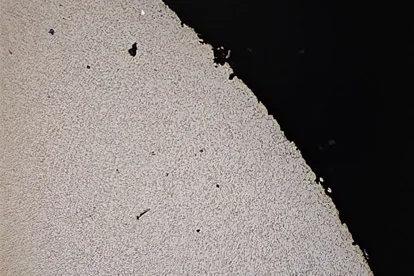
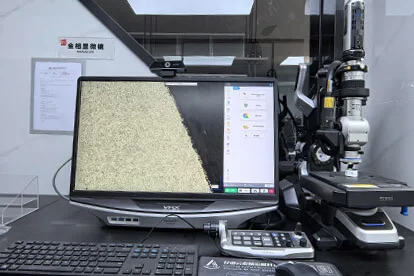
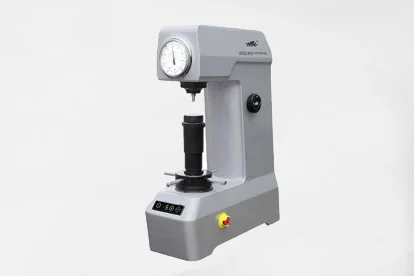
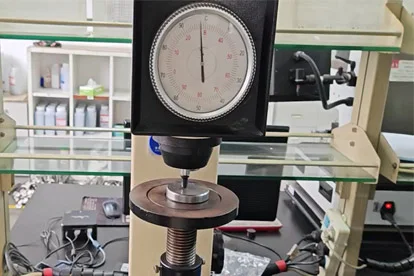
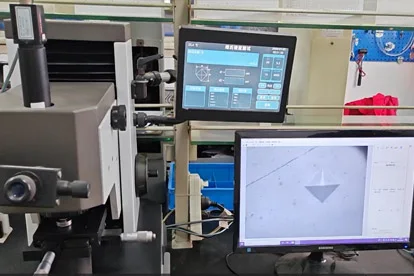
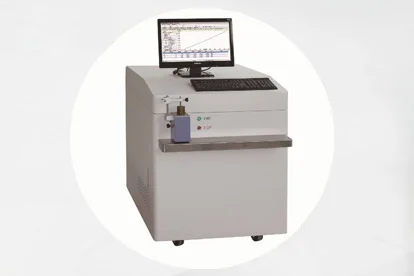
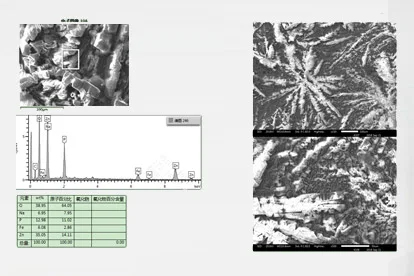
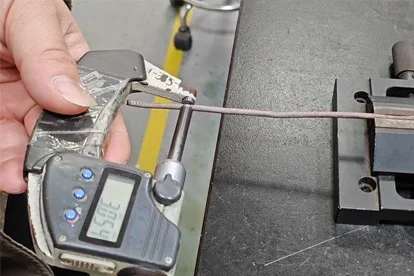
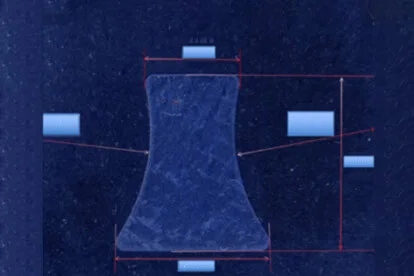
These original catalogue images illustrate equipment and examination methods. They are not batch certificates or proof that every test is required for every Annex A grade. Magnifications and hardness scales retain the original catalogue labels; confirm the actual method, conditions and calibrated scale in the inspection record.
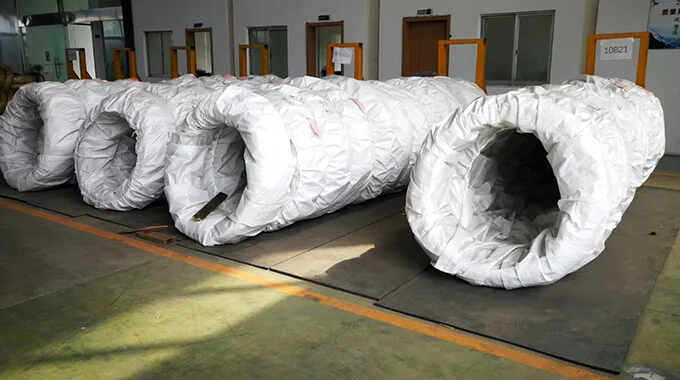
Delivery and packaging
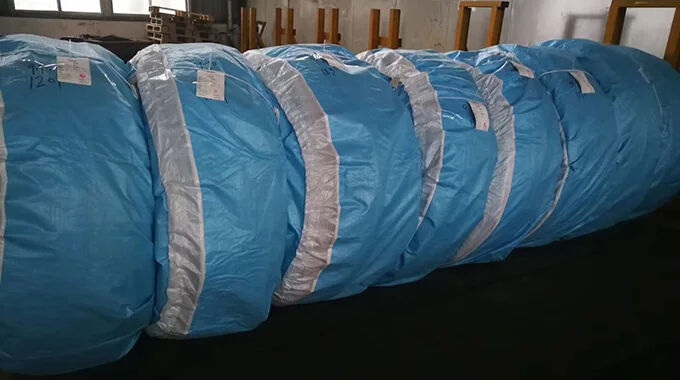
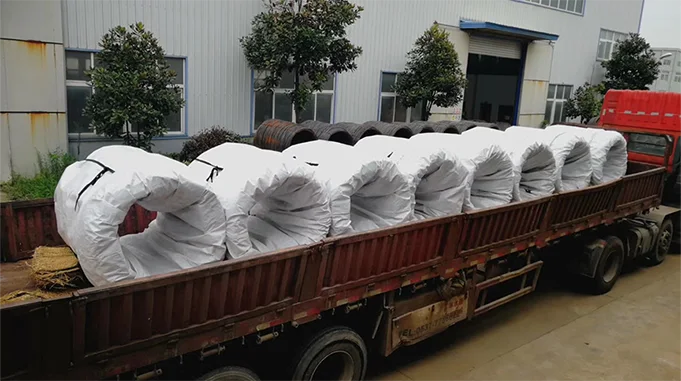
Delivery options in the catalogue include coils, straight lengths and export wooden crates. Protective options include end-face wooden boards, wrapping, PP woven bags, wire racks and pallets. Confirm the selected arrangement in the order. Packaging illustrations do not establish technical compliance or a verified loading record.