
STANDARD FIRST · ENGINEERING FIRST
Cold-Heading Engineering Classroom
Engineering knowledge that connects formal standards, material behavior and cold heading practice.
ALL ARTICLES
Engineering classroom articles
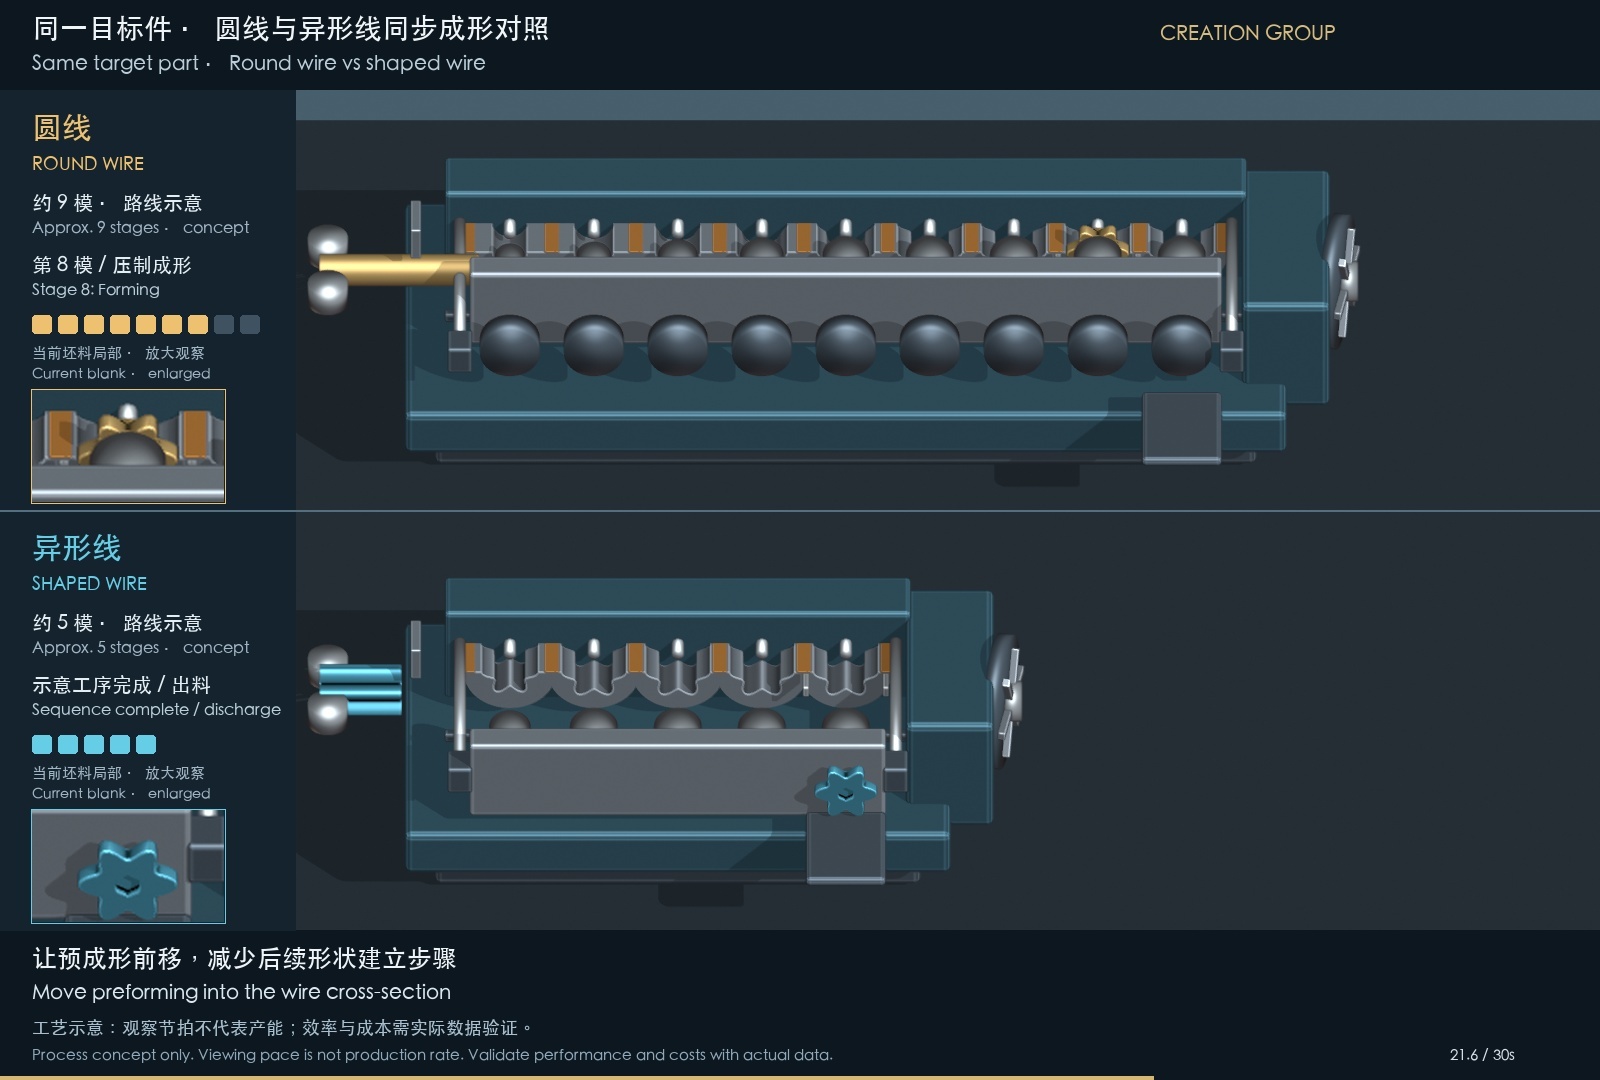
Cold Heading Routes and Cost Comparison
Compare round- and shaped-wire forming concepts at equal conforming output, with capacity checks and input-based material, tooling, equipment and operating costs.
Read article →
Can pickling be skipped before spheroidizing annealing of SCM435 wire rod?
How mill scale can contribute to surface decarburization during the first spheroidizing anneal of SCM435 wire rod, and…
Read article →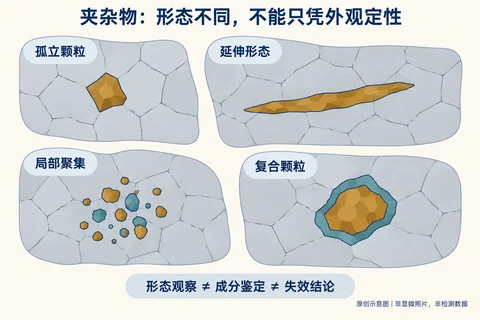
Inclusions and Cold-Heading Cracks: What the Evidence Can Establish
Separate particle observation, standard conformity, crack causation and responsibility. Use traceable sampling, analysis and process evidence before assigning a root cause.
Read article →Why Cold-Heading Wire Often Starts Round
Round wire is versatile. A suitable shaped starting section can shorten demanding flow paths, subject to the actual part, tooling and production validation.
Read article →
Cracks After Cold Heading: What Can Hardness Tell Us?
Original site records show cracked screw heads and an approximately 185 HV0.2 display. The records do not, by themselves, establish a root cause or acceptance limit.
Read article →Softer Wire Is Not Always the Better Cold-Heading Solution
Interpret hardness requests through the actual manufacturing problem, microstructure, coating and later operations; minimum HRB is not a universal objective.
Read article →
BOF and EAF Steelmaking: Route and Quality Are Different Questions
Understand the charge and heat source, verify the steelmaker’s actual route and evaluate the delivered material against the intended product requirements.
Read article →
Why Does Scuffing Persist After a Material Change?
A 20MnB4 tubing-nut case examines die-passage clearance, lubricant condition and filtration, with observations kept separate from confirmed causes.
Read article →
Does a Thin Phosphate Coating Explain Cold-Heading Scuffing?
Coating mass, coverage, adhesion, soap lubrication and deformation history all affect scuffing. A thicker phosphate coating is not a universal remedy.
Read article →Network Cracks in a Bolt Flange: Structure and Hardness Evidence
Customer-supplied SCM435-labelled samples show a near-surface structural difference and higher HV0.1 values; annealing and carburization explanations remain subject to verification.
Read article →
Chapter 10: From Sample Approval to Stable Production
An approved trial establishes a limited material and process result. Preserve the conditions and extend validation across coils, batches and sustained production.
Read article →
S55C Thin-Wall Cold-Forming Case: Material and Production Controls
An anonymized automotive case connects S55C wire condition, coating and batch consistency with thin-wall forming; public dimensions and illustrations are not acceptance records.
Read article →
Chapter 9: Material Suitability Across Cold-Heading Machines
Compare identified material, station samples, operating conditions and repeatable production results when the same part behaves differently on two machines.
Read article →Chapter 8: Part Geometry and the Forming Sequence
Heads, flanges, bores and steps change material flow. Review preforms and station samples to connect the starting wire with the final geometry.
Read article →
Why Can Phosphate-and-Soap Lubrication Fail in Cold Heading?
Residual coating after drawing, adhesion, die-cavity lubricant and forming conditions must be evaluated together; appearance and coating mass alone are insufficient.
Read article →
Chapter 6: How Drawing Changes Cold-Heading Behaviour
Drawing history affects work hardening, directional yielding and later forming. Compare reductions, pass schedules, storage and actual production evidence.
Read article →
Where do surface defects originate, and why do they persist into cold-headed parts?
Trace scabs, laps, cracks and scoring through casting, rolling, handling, pickling, drawing and cold heading. Locate the first appearance using process evidence.
Read article →
Chapter 4: Spheroidization and Actual Cold Formability
Carbide morphology, size, distribution, ferrite condition and representative sampling matter alongside a spheroidization rating and hardness result.
Read article →
Chapter 3: Localized Cracking Within One Material Batch
Representative passing tests can coexist with local damage. Trace the affected coil section and identify where a defect originated and was amplified.
Read article →Chapter 2: What Material Standards Can Establish
Separate product conformity from actual forming validation, including microstructure, drawing history, coatings, equipment and sustained production.
Read article →
Chapter 1: Material Compliance and Cold-Heading Stability
A compliant material specification is the foundation. Part geometry, dies, equipment, lubrication and production conditions also require process validation.
Read article →
ML40Cr and 40Cr: More Than a Grade Prefix
Compare 40Cr and ML40Cr by standard edition, composition, steel quality class, product form and the intended cold-heading route.
Read article →
35CrMo and ML35CrMo: Standards and Cold-Heading Suitability
Compare the stated GB/T 3077, GB/T 6478 and GB/T 28906 editions, with chemistry, product form, delivery condition and cold-heading validation kept distinct.
Read article →
SWRCH10A to SWCH10A: From Wire Rod to Wire
JIS G 3507 distinguishes wire rod from finished wire. The missing R identifies product form and does not, by itself, establish finished-wire conformity.
Read article →
Square-Nut Forming: Why the Starting Wire Section Matters
A SWRCH10A 13.80 mm square-wire example explains how starting geometry can change corner filling; actual benefits require drawing-based trials and production evidence.
Read article →
SUJ2: A Bearing-Steel Grade in the JIS System
SUJ2 is a high-carbon chromium bearing-steel designation. The suffix is a grade identifier, while composition and acceptance requirements come from the product standard.
Read article →
Reading SCM435 in the JIS Steel System
SCM435 is a JIS chromium–molybdenum steel identifier. Check its specified carbon range, delivery condition and product standard rather than infer equivalence from the name.
Read article →
What Do 1022A, 1010A, 1008A and 1006A Mean?
Distinguish SAE J403:2014 grades, JIS SWRCH identifiers and ASTM F2282 IFI designations. An A-suffix label alone does not define a material or approve substitution.
Read article →