
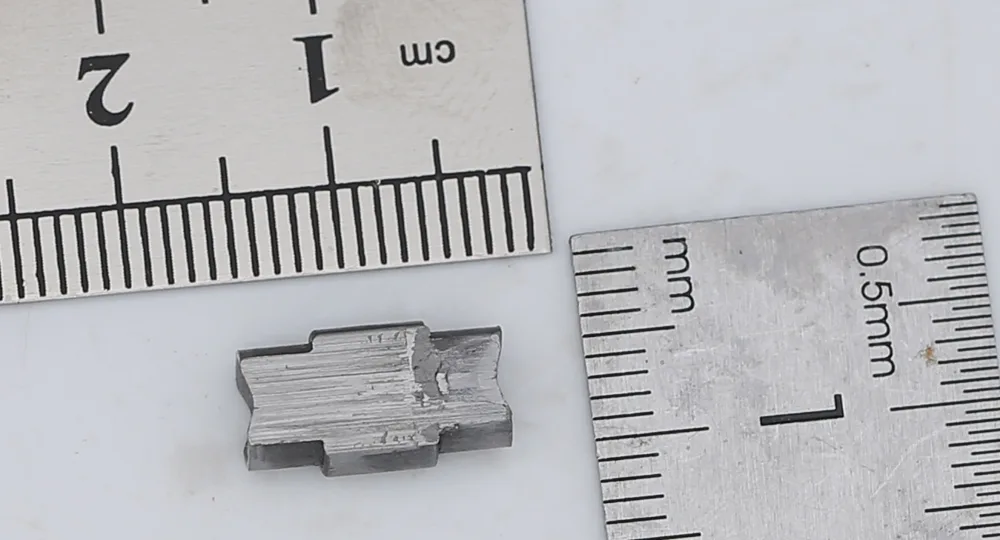
Chemical composition
Cast analysis, mass fraction %. Unspecified values are not zero.
| Element | Mass fraction / % |
|---|---|
| C | 0.35~0.42 |
| Si | 0.8~1.2 |
| Mn | 0.25~0.5 |
| Cr | 4.8~5.5 |
| Mo | 1.2~1.5 |
| V | 0.85~1.15 |
| P | ≤0.03 |
| S | ≤0.02 |
Properties and applicable conditions
| Property | Standard requirements and applicable conditions |
|---|---|
| Annealed hardness HBW / maximum | 229 |
| Hardening test | Austenitizing 1020±10 °C ; oil quenching (standard test) ; tempering 550±10 °C ; hardness≥50 HRC |
Standard reference and ordering limitations
- Cast analysis, mass fraction %. A dash means the standard gives no separate requirement; it does not mean zero.
- Unlisted elements shall not be intentionally added without purchaser consent, except additions needed to finish steelmaking.
- Permissible product-analysis deviations do not expand the default cast-analysis limits.
- Tool-steel classification and hardness depend on application, heat treatment and test conditions; they do not establish cold-heading suitability or guarantee properties in an arbitrary condition.
- Table 6: hot-work tool steels; cast analysis, wt%; P≤.030%, default S≤.020%; for 55NiCrMoV7, note d specifies S≤.030%.
- Unlisted elements shall not be intentionally added without purchaser consent, except to finish steelmaking. Dashes are not entered as zero.
- Annealed and cold-drawn (+A+C) hardness may be 20 HBW higher than annealed (+A) hardness. Hardness values for different conditions must not be interchanged.
Reference: BS EN ISO 4957:2018,Table 6 and notes a–f. Website information does not replace the official standard, order specifications or material certificates.
Illustrative packaging
Product and packaging images are illustrations; they do not identify a heat, stock availability, dimensions or a default delivery method. Confirm product form, delivery condition, packaging and acceptance requirements in the enquiry and order.