产品中心/ISO 4954

MATERIAL DATA · COLD FORMING

31CrMoB2-1 冷镦钢丝

31CrMoB2-1 冷镦钢丝技术资料,执行标准为 ISO 4954。查看当前牌号的化学成分、力学性能及相关技术要求。

供货与技术评审 · 睿雄集团受理本产品的供货与技术评审需求;规格、交货状态、数量和检验文件经评审后按订单技术协议确认。

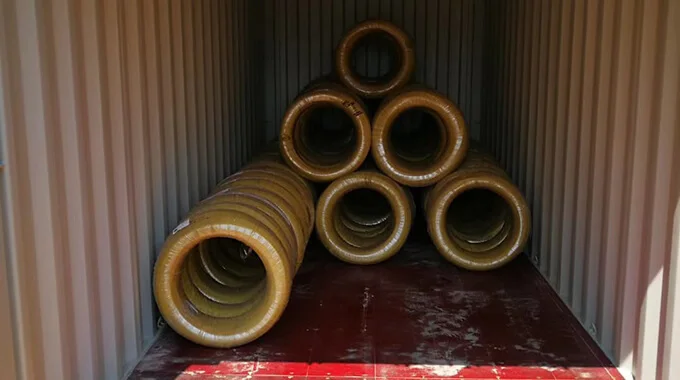
31CrMoB2-1 冷镦钢丝 产品图片
31CrMoB2-1 · 冷镦钢丝
01执行标准ISO 4954
02材料牌号31CrMoB2-1
03材料形态冷镦钢丝
04交货说明按订单技术条件确认

材料技术参数

1.交货条件的组合

表C.1交货时热处理条件的组合、产品形式和适用要求

2.化学组成

表C.3-淬火和回火用硼合金钢牌号的化学成分 (适用于熔炼分析)

Elements not quoted in this table should not be intentionally added to the steel without the agreement of the purchaser,except those intended for finishing the heat.All reasonable precautions shall be taken in order to prevent the addition of such elements from scrap or other materials used in the production process,which can affect the hardenability, mechanical properties and applicability To improve the performance of cold heading,it is possible to add Al:0,020 %to 0,050 %.
a b
Maximum values unless otherwise indicated. In the case of steels with hardenability requirements (see Table C.8),minor deviations from the specified limits are permitted (with the exception of sulfur and phosphorus)   c   Lower silicon contents may be agreed at the time of ordering,in which case due consideration should be given to the effects that could result for what concerns the specified properties such as,for example,hardenability. d Where a maximum chromium content of 0,30 %is specified,a minimum level may also be agreed at the time of enquiry and order e  In order to obtain a core hardening for the steel grade 30MoB1,the lower limit of Cr shall be 0,15 %and may be agreed at the time of enquiry and order.For certain applications, the higher limit for Cr may also be lowered by agreement at time of enquiry and order.

Steel name b% mass fraction a
CSI cMnPSCr dMoBCu
31CrMoB2-10,28 to 0,330,300,90 to 1,200,0250,0250,40 to 0,550,10 to 0,150,0008 to 0,0050,25

3.力学性能

表C.6-硼合金钢牌号的力学性能

Steel nameDiameterDelivery condition
+AR or +PE+AC or +AC+PE+AR+C+AR+C+AC+AR+C+AC+LC+AC+C
above mmup to mmRm max. MPaZ min. %Rm max. MPaZ min. %Rm max MPaZ min. %Rm max. MPaZ min. %Rm max. MPaZ min. %Rm max. MPaZ min. %
31CrMoB2-125———5706361061———
540——57061—550635906169056
It should be recognized in the +AR condition that the tensile strength values are not compatible with the whole range of composition given in T able C. 3 for a steel grade,Care should be taken that,depending on diameter and composition supplied,the tensile strength values are compatible with the hardenability requirements.

4.淬透性要求

表C.8-具有标准淬透性的硼合金钢等级的硬度限值 (H级)

表C.10-芯部硬度试验中至少应获得90% 马氏体的最大直径 (+ CH等级)

使用与订购说明

化学成分、力学性能、交货状态及其他技术要求应以现行有效标准、客户图纸和订单技术协议为准;网页资料不替代正式质量证明文件。

询盘建议提供资料

碳当量计算器 — 31CrMoB2-1

依据: ISO 4954

化学成分依据: ISO 4954:2018

按所列标准原文转录

来源原文

Table C.3

IIW / CEV

CEV = C + Mn/6 + (Cr + Mo + V)/5 + (Ni + Cu)/15已知项贡献,非完整值: 0.5300–0.6867

缺少元素: V, Ni

IIW/CEV:碳钢和低合金钢的焊接性初筛。

Pcm (Ito–Bessyo)

Pcm = C + Si/30 + (Mn + Cu + Cr)/20 + Ni/60 + Mo/15 + V/10 + 5B已知项贡献,非完整值: 0.3557–0.4750

缺少元素: Ni, V

Pcm:主要适用于低碳低合金钢;尤其 C 超过 0.11% 时,须另行确认适用性。

CET

CET = C + (Mn + Mo)/10 + (Cr + Cu)/20 + Ni/40已知项贡献,非完整值: 0.4000–0.5050

缺少元素: Ni

CET:铁素体钢焊接预热评估,须核对 EN 1011-2 的适用条件。

单侧上限表示从 0 到该上限;只有下限时不能确定上界。缺项未知,不按零处理。标准极限组合值不是炉批实测值。

碳当量辅助评估焊接性,不代表冷镦、紧固件强度或焊接工艺获准。上述公式不直接适用于不锈钢、铸铁及有色金属。

方法引用: TWI

碳当量计算器 →

提交该材料技术询盘

联系技术团队 →

材料参考资料

同牌号参考不代表标准等同、实际供货或替代批准。

WhatsApp 技术询盘 →